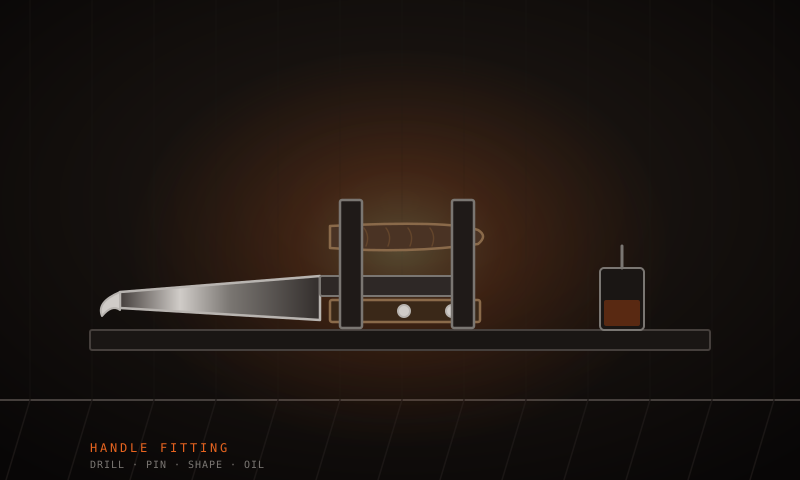
The handle is the part of a knife that gets used most and looked at first, and it is also the part beginners rush. A blade that is ground and heat treated beautifully can be ruined by a handle that is too fat, too smooth or glued on crooked. The good news is that handles are forgiving: most mistakes can be sanded away, and the material is cheap enough to redo.
Handle work is mostly about preparation. If the tang is flat, the holes are drilled straight, the scales sit flush and the epoxy has something to grip, assembly is easy. If any of those are wrong, no amount of clamping pressure will fix it. Work through the preparation carefully and the assembly itself takes twenty minutes.
Handle materials and what they do
Handle materials fall into three broad groups: hardwoods, stabilized wood and synthetic laminates. Hardwoods like walnut, maple, ash and oak are inexpensive, easy to shape and warm in the hand. They move with humidity, which means a handle that fits perfectly in summer may show a tiny step at the tang in winter.
Stabilized wood has been impregnated with resin under vacuum, which fills the pores and makes it harder, more stable and more water resistant. It costs more and it is worth it for a knife that will see real use. Synthetic materials such as micarta and glass-reinforced laminates are dimensionally stable, tough and effectively waterproof. They are harder on belts and they dull files quickly, but they will not shrink or split.
- Walnut and maple: inexpensive, easy to shape, warm in the hand, but they move slightly with humidity.
- Stabilized wood: resin-impregnated, harder and more stable, and much more resistant to moisture.
- Micarta and similar laminates: dimensionally stable and tough, but abrasive on belts and files.
- Horn and bone: traditional and attractive, but they can be brittle and they smell strongly when sanded.
- Avoid soft, open-grained woods and any material with hidden voids or checks near the tang.
| Material | Stability | Workability | Best for |
|---|---|---|---|
| Walnut, maple | Moves slightly with humidity | Easy to shape and sand | Traditional working knives |
| Stabilized wood | Very stable once cured | Moderate, resin dulls tools | Everyday use and wet climates |
| Micarta laminates | Effectively waterproof | Abrasive on belts and files | Hard-use and field knives |
| Horn and bone | Can become brittle over time | Dusty and strong-smelling to sand | Traditional and display pieces |
Preparing the tang and drilling
The tang needs to be flat. If it is forged it will not be, and if it is a hidden tang it may be tapered. Flatten the visible section on a belt or a flat plate, check it against a straightedge, and make sure the shoulders are square where the handle material will meet them. A gap at the shoulder is the most visible flaw in a finished knife.
Drill the pin holes while the tang is soft, before heat treatment if you can. Mark them, center punch them, and drill on a press at slow speed with a little cutting fluid. Then transfer the holes to the scale material by clamping the scale to the tang and drilling through the existing hole. That guarantees alignment far better than measuring and hoping.
Flatten and square the tang
Work the tang flat on a belt or a plate, then check with a straightedge. Square the shoulders so the scale material sits against them with no visible gap.
Mark and drill the pin holes
Space them evenly and keep each hole at least its own diameter away from the edge of the tang. Center punch every one so the bit does not walk on the curved surface.
Clamp and transfer
Clamp one scale to the tang and drill through the tang holes into the scale, then flip and repeat. This guarantees the holes line up without any measuring at all.
Rough the mating surfaces
Scuff the tang and the inside of both scales with coarse paper. Epoxy bonds to a scratched, clean surface far better than to a polished one.
Degrease everything
Wipe the tang and the scales with acetone or alcohol and let them dry. Oil from your fingers is enough to weaken a glue joint, and you will not see the failure until the handle comes loose.
Epoxy, clamping and cleanup
Use a proper two-part epoxy and mix it thoroughly for at least the time stated on the label. Mixing for ten seconds is the most common cause of a joint that never fully cures. Work in a ventilated space, wear gloves, and have everything laid out before you mix, because once it is mixed you have limited working time.
Apply epoxy to both surfaces, not just one. A thin, even coat on the tang and on each scale gives the best joint. Slide the scales into place, insert the pins, and clamp. Clamping pressure should be firm but not extreme, enough to close the gap and squeeze a little epoxy out but not enough to starve the joint. Wipe the squeeze-out while it is still soft, because once cured it is much harder to remove without scratching the material.
Pins, bolts and peening
Pins hold the scales mechanically as well as providing decoration. The rule that catches beginners is this: brass pins should be slightly proud of the surface and peened, not left flush. Peening spreads the pin head into the surrounding material, which locks the scale in place and creates the traditional hammered look. A pin cut flush and polished looks neat in a photograph and does much less work.
The exception is Corby-style or Loveless bolts, which are designed to be screwed and glued in place and then finished flush. Those are mechanical fasteners rather than peened pins, and they should be installed the way they are made: drilled to the specified size, epoxied, tightened, then ground flush with care not to burn the surrounding material.
Cut the pins slightly long
Leave about 1.5–2 mm of pin standing proud on each side. Too short and you cannot peen it. Too long and it bends instead of spreading.
Peen with light, rapid blows
Use a small hammer with a slightly domed face and tap around the pin head in a circle. Light and fast spreads the head. Heavy blows bend the pin or crack the scale.
Alternate sides
Peen a little on one side, then the other, so the pin stays centered and does not bow the tang. Work gradually and check the fit as you go.
Grind flush and blend
Once the head has spread and locked the scale, grind the remaining proud material down and blend it into the surrounding surface without overheating the handle.
Check for movement
Before you commit to finishing, flex the handle gently and look for any gap opening at the shoulder. A loose scale is fixable now and a disaster later.
Shaping the handle
Shape the handle with the blade masked and the knife held safely. The goal is a handle that fills the hand without being fat, with a swell where your palm sits and a taper toward the front so your fingers can wrap comfortably. Most beginner handles are too thick, because material feels safe and removing it feels risky.
Work from coarse to fine. A 60 or 80 grit belt shapes quickly, a 120 belt refines the shape, and hand sanding from 220 up to 800 or 1000 gives you a surface worth looking at. Keep the handle symmetrical, check it from above and below as you go, and remember that a handle which looks right in a photograph can still be uncomfortable in the hand. Hold it, cut with it, and adjust.
- Round the front of the handle where your index finger sits. A sharp corner there is the most common comfort failure.
- Leave a slight swell at the palm and taper toward the front so the hand can close naturally around it.
- Keep the handle symmetric. Check from the top, the bottom and both sides as you shape it.
- Keep the spine of the tang flush or very slightly proud at the top. A step there catches your hand constantly.
- Sand with the grain where the material has one, especially on wood, or you will leave visible cross scratches.
Finishing and checking the fit
Finishing is what separates a homemade handle from a made handle. Sand progressively, remove all the previous grit scratches, and do not rush the last two stages. On wood, raise the grain with a damp cloth, let it dry, and sand again before the final coat. That stops the surface from feeling rough after the first use.
For an oil finish, apply thin coats of a hardening oil and let each one dry, building the surface slowly. For a film finish, use a thin wipe-on product and many thin coats rather than one thick one. Whichever you choose, finish the handle before you sharpen the blade, so you are not handling a razor edge while you work.
Sand progressively
220, 320, 400, then 600 or 800. Do not skip grits, and change sanding direction with each grit so you can see when the previous scratches are gone.
Raise the grain on wood
Wipe with a damp cloth, let it dry completely, then sand lightly again. This lifts crushed fibres so the final finish stays smooth instead of feeling fuzzy after use.
Apply the finish in thin coats
Thin coats, fully dried between applications. One thick coat stays soft underneath and will look worse in a month than four thin ones.
Blend the finish at the tang
Where the handle meets the metal, take the finish right up to the shoulder and wipe away any that creeps onto the blade or the ricasso.
Check the whole knife
Flex the handle, look for gaps, confirm the blade sits in line with the handle, and make sure the pins or bolts are tight before you call it done.
Key takeaways
- Flatten and square the tang, drill the pin holes in soft steel, and transfer them to the scales by clamping and drilling through.
- Scuff and degrease both mating surfaces. Epoxy grips a scratched, clean surface and fails on a polished, oily one.
- Brass pins should sit slightly proud and be peened. Corby-style and Loveless bolts are the exception and finish flush.
- Most beginner handles are too thick. Aim for a palm swell and a taper toward the front, then test it in the hand.
- Sand progressively, raise the grain on wood, and build the finish in thin coats before you sharpen the blade.
Frequently asked
Two pins are enough for most knives, and three are common on longer handles. The pins resist shear and the epoxy does the rest. What matters more than the count is that the holes are drilled straight and the pins are peened or tightened properly, because a loose pin lets the scale move and eventually opens a gap.
No, not for the main bond. Cyanoacrylate is brittle, has poor gap-filling ability and fails under the moisture and shock a knife handle sees. It is useful for sealing a small crack or holding a scale in place while you drill, but the structural joint should be a two-part epoxy mixed thoroughly and given its full cure time.
Usually because the tang was not flat or the shoulders were not square, so the scale only touched in a few places. Epoxy bridges small gaps but not large ones, and movement opens them over time. Flatten the tang against a straightedge, square the shoulders, and make sure the scale sits down with no rocking before you glue.
Related articles
Blade Grinding: From Profiling to Sharpening
Grinding is where a knife is won or lost. This covers belt selection and grit progression, setting bevels and plunge lines cleanly, and taking an edge from a 36 grit belt all the way to an 8000 grit stone.
Making a Leather Sheath: Step by Step
A sheath is a fitted leather case made around the knife, not a pouch the knife is dropped into. This walks through the pattern, the welt, wet forming and the stitching that holds it together.
Knife Maintenance and Sharpening
An edge fails in predictable ways and each one has a different fix. This covers the angles for different knives, a stone progression that works, and how to keep a carbon steel blade from rusting.